
Buy Non Serrated Flange Nuts Manufacturer & Manufacturers
Precision DIN 6923 / ISO 4161 Non-Serrated Flange Nuts: Superior Load Distribution, Surface Coating Preservation, and Mechanical Reliability for Industrial, Solar PV, and Heavy Infrastructure Sectors.
Featured High-Performance Industrial Fasteners & Mounting Modules
Direct from factory production lines in Yongnian, China’s Fastener Capital. Engineered to pair seamlessly with non serrated flange nut assemblies for solar racking, steel frameworks, and mechanical arrays.
-
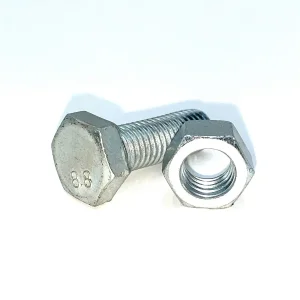
Buy High-Strength Hex Bolt from China Factory - Reliable Fastening Solutions by Trusted Suppliers Manufacturers, Suppliers
-
Best China Suppliers Three-Hole Mounting Connector for Solar PV Systems - Durable Aluminum Alloy Factory Product Manufacturers, Factories

-
China High-Strength Hex Bolt from China Factory - Reliable Fasteners from Trusted Suppliers Company, Companies
-
China Durable Solar PV Mounting Purlin Connector Supplier and Factory in China - High Strength and Anti-Corrosion Manufacturers, Companies

-
China Heavy-Duty Hot-Dip Galvanized Hex Bolts from China Suppliers | Durable Factory Quality for Outdoor Use Supplier, Company

-
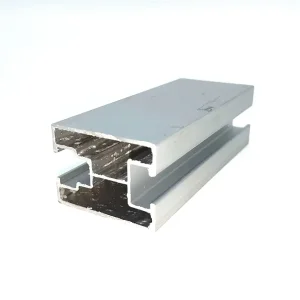
China High-Strength 3040 Reinforced Aluminum Guide Rail for Solar Panels - Trusted China Suppliers & Factory Solutions Companies, Products
-
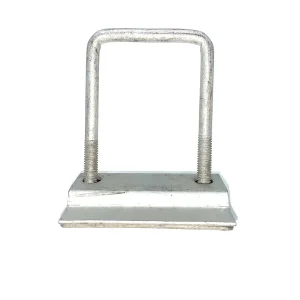
Best China Suppliers Factory High-Strength Double-Hole Pressure Plate for Solar PV Mounting Systems Factories, Product
-
Best High-Strength Hex Bolt - Durable Carbon Steel Fasteners from China Suppliers & Factory for Machinery and Construction Supplier, Products
Global Commercial & Industrial Landscape of Non Serrated Flange Nuts
In advanced structural mechanical design, the selection between serrated and non-serrated flange nuts represents a fundamental engineering decision. Non serrated flange nuts—characterized by a seamless, flat flange integrated with a standard hex nut body—act as a high-integrity, unified fastener-washer system.
Surface Protection & Anti-Galling
Unlike serrated alternatives that actively bite into the substrate and tear protective coatings, non serrated flange nuts apply smooth, uniform compression. This proves indispensable when fastening painted sheet metals, hot-dip galvanized steel, powder-coated enclosures, and anodized aluminum profiles, preventing galvanic acceleration and premature rust.
Precision Clamping Load Distribution
The widened bearing area minimizes localized contact stress over oversized, slotted, or misaligned clearance holes. By dissipating tension over an expanded footprint, these fasteners eliminate the requirement for separate loose flat washers, cutting component counts and slashing assembly line labor cycle times by up to 28%.
Predictable Torque-Tension Relationship
Serrations cause friction variations during seating, resulting in erratic clamp loads. Non serrated flange nuts deliver consistent nut factor (K-factor) coefficients. This stability allows torque-controlled multi-spindle automated assembly tooling to achieve pinpoint bolt preloads without thread damage or stripping.
Standard Specification Matrix: Non-Serrated Flange Nuts
Manufactured according to DIN 6923, ISO 4161, and ASME B18.16.4M dimensional profiles, compatible across industrial fastening operations worldwide.
| Metric Nominal Thread | Pitch (Standard Metric) | Flange Diameter (dc max) | Width Across Flats (s max) | Overall Height (m max) | Proof Load Class 8 (kN) | Proof Load Class 10 (kN) |
|---|---|---|---|---|---|---|
| M5 | 0.8 mm | 11.80 mm | 8.00 mm | 5.00 mm | 12.2 kN | 14.8 kN |
| M6 | 1.0 mm | 14.20 mm | 10.00 mm | 6.00 mm | 17.2 kN | 20.9 kN |
| M8 | 1.25 mm | 17.90 mm | 13.00 mm | 8.00 mm | 31.8 kN | 38.1 kN |
| M10 | 1.5 mm | 21.80 mm | 15.00 mm | 10.00 mm | 50.5 kN | 60.3 kN |
| M12 | 1.75 mm | 26.00 mm | 18.00 mm | 12.00 mm | 74.2 kN | 88.5 kN |
| M16 | 2.0 mm | 34.50 mm | 24.00 mm | 16.00 mm | 141.0 kN | 168.0 kN |
Sector-Specific Engineering Application Scenarios
How global procurement leaders and structural designers leverage non serrated flange nuts across high-demand industrial installations.
Solar Photovoltaic Tracker & Racking
In single-axis tracker torque tubes and extruded aluminum rails, serrated nuts scratch anodized and zinc-aluminum-magnesium (ZAM) coatings, accelerating rust. Non serrated flange nuts distribute clamping evenly across thermal expansion slotted holes without biting through coatings, maintaining cathodic protection integrity for 25+ years.
Automotive Powertrain & EV Battery Enclosures
Aluminum battery enclosures and automotive subframes demand smooth seating surfaces to avoid localized micro-cracking and galvanic corrosion. Using stainless steel (A2/A4) or geometrically coated Class 10 non-serrated flange nuts ensures stable clamping across variable dynamic vibration loads.
Industrial HVAC & Prefabricated Steel Frames
Modular building and ductwork systems require swift connection speeds. With broad integrated washers, workers can secure connections without holding loose washers behind slotted bracket holes, optimizing site assembly speeds across high-wind seismic assemblies.
Fastener Technology Roadmap: Advancing Surface Science & Preload Control
The fastener industry is evolving beyond traditional hot-dip galvanizing and electro-zinc plating toward eco-friendly, ultra-durable thin-film passivation technologies.
Phase 1: Zinc Flake & Geomet Coatings
Eliminating hydrogen embrittlement risks in high-tensile Class 10.9 assemblies. Non-electrolytic zinc flake coatings supply 1,500+ hours of ASTM B117 salt spray endurance without thick thread build-up, maintaining free thread engagement on automated feeding systems.
Phase 2: Integrated Friction-Modifier Topcoats
Integrating synthetic wax-based lubricated topcoats directly over the non-serrated flange face. This guarantees a tightly controlled coefficient of friction (μ = 0.10 – 0.16), standardizing tightening torque accuracy on critical installations.
Phase 3: Smart Fastener Cold-Forming
Utilizing high-speed 6-station progressive cold-forging presses coupled with in-line eddy current crack detection and optical vision sorting, guaranteeing a defect rate below 50 PPM for automated robotic assembly lines.
Enterprise Supply Chain Resilience: Direct-from-Source Procurement
Handan Youlong Fastener Co., Ltd. sits in the heart of Yongnian District, China's Fastener Capital. We provide end-to-end manufacturing, custom drawing adaptation, and full traceability for international engineering contractors, wholesalers, and OEMs.
Vertical Steel Supply Integration
Direct supply partnerships with major regional steel mills ensure tight control over raw carbon steel rod (10B21, 35K, 45#) and stainless coils (304/316), shielding our partners from global spot-market price volatility and raw material delays.
Exacting Quality & In-House Lab Testing
Every production lot undergoes rigorous mechanical testing: Rockwell hardness (HRC), Vickers microhardness, tensile and proof load testing, alongside cyclic salt-spray corrosion chamber evaluations to ensure 100% standard compliance before shipment.
Comprehensive Documentation & Traceability
Full EN 10204 3.1 Mill Test Certificates (MTC), chemical spectrometry breakdowns, coating thickness x-ray reports, and Certificate of Origin documents accompany every sea and intermodal rail shipment.
Frequently Asked Questions: Non Serrated Flange Nuts
Essential technical, manufacturing, and procurement guidance for mechanical engineers and supply chain directors.
What is the primary operational difference between serrated and non serrated flange nuts?
When should engineers specify a non serrated flange nut instead of a standard hex nut and separate washer?
What steel grades and material alloys are available for volume manufacturing?
What surface treatments provide the best corrosion protection for outdoor solar structures?
How can overseas buyers verify factory compliance and inspect batches prior to dispatch?
High-Integrity Fasteners, Anchor Bolts & Structural Hardware
Complete structural assembly packages available for utility solar fields, prefabricated commercial warehouses, and heavy engineering facilities.
-
Buy Heavy-Duty Stainless Steel Expansion Bolt | China Suppliers & Factory for Reliable Fastening Solutions Company, Products

-
China High-Strength 3040 Reinforced Aluminum Guide Rail for Solar PV Systems - Leading China Suppliers & Factory Factory, Product
-
Best High-Strength Solar PV Mounting Aluminum Alloy Base - Reliable Support from China Suppliers & Factory Factories, Company

-
China High-Quality Stainless Steel Self-Drilling Screws - China Suppliers & Factory for Metal, Plastic, and Wood Fastening Manufacturers, Product
-
Buy China Factory Suppliers Stainless Steel Hex Socket Combination Bolt with Built-in Washer, Anti-loosening and Corrosion Resistant Manufacturer, Companies
-
China Stainless Steel Self-Drilling Screw Manufacturer, Manufacturers
-
China Heavy-Duty Hot-Dip Galvanized Carriage Bolt - China Suppliers & Factory for Superior Corrosion Resistance Supplier, Factories

-
Best High-Strength Hex Socket Bolt Suppliers in China - Durable Carbon Steel Factory Fasteners for Machinery & Construction Company, Product
