Engineered Structural Fasteners & Support Systems
Explore high-integrity fastening components manufactured under rigorous metallurgical quality controls in Handan, China's premier fastener and ground-support engineering hub.





Engineering Mechanics of Self-Drilling Anchor (SDA) Systems
Overcoming borehole collapse in loose gravel, weathered sandstone, fractured metamorphic rock, and high water-inflow conditions with continuous hollow-core reinforcement.
Single-Step Drilling & Grouting
Traditional ground anchoring mandates a three-stage cycle: casing installation, drill-string extraction, and anchor rod insertion. In fractured or collapsible geology, borehole walls disintegrate instantaneously upon casing removal. Self-Drilling Rock Bolts (SDRB) consolidate drilling, flushing, and high-pressure cement grouting into an uninterrupted continuous operation, driving installation cycle times down by up to 60%.
Continuous Hollow-Core Bar Mechanics
The cold-drawn, micro-alloyed structural steel hollow core functions simultaneously as the drill rod, the grout discharge conduit, and the permanent tensile/shear tendon. Continuous external rope (R) or trapezoidal (T) thread profiles maximize bonding mechanical interlock between the anchor body, the primary grout column, and the surrounding geological stratum.
Sacrificial Bit Geometries
Matched to geological hardness (Mohs scale 2 through 8+), engineered sacrificial drill bits—ranging from hardened carbon-steel cross bits to tungsten carbide (TC) button bits—remain anchored at the toe. Flushing apertures allow pressurized water, bentonite slurry, or dynamic grout to evacuate drill cuttings efficiently while penetrating fissured formations.
Standard Thread Geometry & Geotechnical Load Matrix
Precision engineered hollow bars fabricated from high-grade micro-alloy steel (such as 40Cr, 30CrMo, or modified structural steels), conforming to ISO, EN, and ASTM standards.
| Profile Specification | Outer Diameter (mm) | Inner Diameter (mm) | Yield Load (kN) | Ultimate Tensile Load (kN) | Standard Weight (kg/m) | Typical Ground Application |
|---|---|---|---|---|---|---|
| R25N (Rope Thread) | 25.0 | 14.0 | 150 | 210 | 2.30 | Mining Roof bolting, spiling |
| R32N / R32S | 32.0 | 18.5 | 230 / 280 | 280 / 360 | 3.40 | Tunneling Forepoling, slope nails |
| R38N (Heavy Core) | 38.0 | 19.0 | 400 | 500 | 6.10 | Foundation Micropiles, high shear nails |
| R51L / R51N | 51.0 | 36.0 / 33.0 | 450 / 630 | 550 / 800 | 7.90 | Civil Deep Pit Tieback anchors, retaining walls |
| T76N / T76S (Trapezoidal) | 76.0 | 52.0 / 48.0 | 1,200 / 1,600 | 1,600 / 1,900 | 18.8 | Heavy Infrastructure Avalanche barriers, bridge piers |
| T111L / T111N | 111.0 | 80.0 / 67.0 | 2,400 / 3,100 | 3,000 / 3,900 | 38.2 | Marine & Dam Deep anti-flotation, dam remediation |
Macro Industry Solutions: Mission-Critical Ground Reinforcement
How engineering procurement managers, structural consultants, and tunneling joint ventures deploy our self-drilling anchor systems under severe geotechnical stress.
Tunneling & Underground Caverns
In New Austrian Tunnelling Method (NATM) and umbrella pipe roofing, SDRB hollow bars provide forward ground stabilization (spiling). Pressurized grout consolidates surrounding shear fault zones, establishing a structural arch ahead of tunnel boring or drill-and-blast advance.
Slope Stabilization & Soil Nailing
For highway cuts, railway embankments, and landslide remediation zones, self-drilling rock bolts are driven through colluvium, debris piles, and loose scree. Combined with wire mesh and shotcrete facings, they pin potential slip planes with uncompromising shear resistance.
Micropiling & Deep Excavations
In restricted urban basements or retrofitting historic foundations, large hollow bars (such as R51 or T76) operate as injection micropiles. They withstand both compressive and uplift loads while resisting active lateral earth pressures on secant or soldier-pile retaining walls.
Wind & Solar Renewable Energy
Wind turbine gravity base anchors and utility-scale solar PV arrays installed across fractured mountainous or karst topography leverage SDA systems for bedrock anchoring, neutralizing high wind uplift, seismic overturning moments, and dynamic fatigue cycles.
China Factory 4.0: Supply Chain Resilience & Handan Cluster Advantage
Headquartered in Yongnian District, Handan City—internationally celebrated as China's Fastener Capital—Youlong leverages unmatched upstream raw material integration, smart heat-treatment lines, and automated cold-drawing metallurgy.
Raw Material Upstream Synergy
Located directly adjacent to premier northern steel mills (including HBIS Group), our manufacturing complex secures custom billet heats with strictly verified chemical properties (low sulfur, controlled phosphorus, and customized manganese-vanadium ratios). This eliminates middleman markups and guarantees trace-level metallurgical consistency across 10,000-tonne rolling campaigns.
Continuous Induction Heat Treatment
Achieving structural toughness without brittleness requires specialized thermal control. Our facility utilizes automated continuous medium-frequency induction heat-treatment and controlled atmospheric quenching-and-tempering lines. This yields a fine martensitic-bainitic grain structure capable of withstanding percussive drilling impact without fatigue fracturing.
CNC Precision Thread Rolling & Machining
Rather than cut threads that disrupt grain flow and create notch-stress concentrations, our anchor profiles are cold rolled using high-tonnage multi-axis CNC machines. The cold-working process burnishes the root fillets, work-hardens surface threads, and enhances fatigue endurance limits against extreme cyclical rotary-percussive stresses.
Global B2B Sourcing: Mitigating Total Cost of Ownership (TCO)
Strategic buying guidelines for geotechnical contractors, overseas trading entities, and project developers seeking verified mill quality without project downtime.
Batch Certification & EN 10204 3.1
Never accept unverified commercial steel bars for permanent civil support. Factory procurement contracts must specify EN 10204 Type 3.1 Mill Inspection Certificates validating heat chemical analysis (C, Si, Mn, P, S, Cr, Mo, Ni), tensile elongation ($A_{5}$ or $A_{10}$), upper yield point ($R_{eH}$), and Charpy V-notch energy absorbsion.
Optimized Packaging & Ocean Logistics
Hollow bars are bundled in hexagon-strapped packs with thread protector caps and anti-rust hydrophobic wraps. Palletized couplers, hex nuts, spherical washers, and drill bits are crated in seaworthy, fumigated wooden cases tagged with barcoded SKU tracking to ensure flawless inventory handling at destination ports.
Coupler Interlock & Energy Transmission
A chain is only as strong as its link; a rock bolt string is only as sound as its internal coupler. Our internally threaded, center-stopped alignment couplers ensure full face-to-face contact of mating hollow bars. This eliminates kinetic dampening, maximizing stress wave transmission from hydraulic drifter to drill bit.
Localization, Standards Compliance & Advanced Anti-Corrosion Systems
Ground support systems face extreme underground chemical exposure—including acid mine drainage, chlorides, and groundwater sulfates. We engineer layered defensive barriers.
International Regulatory Frameworks
Our engineering design files and physical quality assurance testing align strictly with international building codes, including European standard EN 14490 (Execution of Special Geotechnical Works: Soil Nailing), EN 14199 (Micropiles), ASTM A615 / A615M, and US Federal Highway Administration (FHWA-NHI-14-007) soil nail design manuals.
Hot-Dip Galvanizing (ISO 1461 / ASTM A123)
For permanent installations requiring a 50 to 100-year design life in moderately aggressive soils, hollow bars undergo hot-dip galvanizing after thread rolling. The molten zinc bath produces a multi-layered iron-zinc alloy coating exceeding 85 μm (610 g/m²), offering sacrificial cathodic defense against micro-pitting and electrochemical cell attack.
Duplex Epoxy & Double Corrosion Protection
In high-stray-current marine ports, saline mud flats, or acidic tailings facilities, we engineer Fusion-Bonded Epoxy (FBE) coatings or pre-grouted corrugated polyethylene (PE/PP) ducting sleeves. This delivers certified Class I Double Corrosion Protection (DCP) ensuring zero ingress of corrosive elements to the primary load tendon.
Technology Roadmap: Intelligent Ground Support & Low-Carbon Steel
Pioneering the convergence of structural IoT sensors, autonomous bolting automation, and low-carbon metallurgical processes.
Smart IoT Fiber-Optic Strain Sensing
Future subterranean excavation demands real-time structural intelligence. Youlong R&D is collaborating on integrating embedded Fiber Bragg Grating (FBG) optical sensors along the internal lumen of hollow bars. This transforms static rock bolts into active structural health monitors, transmitting continuous real-time load, deformation, and axial load distribution data to cloud BIM models.
Robotic & Autonomous Rig Compatibility
As major underground mining and civil tunneling transit toward automated, unmanned drill rigs (Sandvik, Epiroc, Normet), rock bolt tolerances must satisfy sub-millimeter indexing criteria. Our automated CNC threading lines achieve ultra-tight concentricity and chamfered thread entries, preventing robotic carousel feed jams and cross-threading errors.
Hydrogen-Direct Reduced Green Steel
To support our international clients' Scope 3 carbon reduction mandates, our production matrix is piloting electric arc furnace (EAF) melts utilizing green-hydrogen direct reduced iron (DRI). This progressive roadmap targets a 45% reduction in embodied carbon per linear meter of ground anchor by 2030 without sacrificing metallurgical yield strength.
Frequently Asked Technical Questions
Definitive technical and commercial answers addressing common engineering challenges in hollow anchor specification, drilling rates, and international delivery.
R-thread profiles (such as R25, R32, R38, R51) utilize a rounded thread profile optimized for standard rotary-percussive drilling and ease of field coupling. They offer high grout-interlock surface areas and can be connected smoothly under dirty, site-mixed slurry conditions. T-threads (such as T76, T111) feature a robust trapezoidal thread form designed for larger borehole diameters and heavy industrial loads. T-threads provide higher moment and shear resistance, making them ideal for heavy micropiling and high-tonnage tieback systems.
For concurrent drilling and flushing, an initial lean cement grout or water flush is typically used to discharge cuttings. For the final anchoring column, standard Portland cement (OPC) mixed to a water-cement ratio between 0.40 and 0.50 (by weight), often with non-shrink plasticizing additives, is recommended. Grouting pressures typically range from 0.5 to 2.5 MPa (5 to 25 bar), depending on the fracturing and permeability of the formation, ensuring complete penetration into surrounding fissures.
Unlike budget producers who machine cut threads, Youlong utilizes specialized precision cold-rolling lines on normalized micro-alloy hollow billets. Cold rolling preserves continuous, uninterrupted grain boundaries along the thread roots, significantly elevating yield shear capacity and fatigue resistance. Furthermore, our couplers are designed with precision internal center stops, ensuring 100% axial contact between bar faces so percussion energy transfers directly bar-to-bar rather than through thread teeth.
Yes. We manufacture a comprehensive matrix of sacrificial drill bits: cross-cut steel bits for soft-to-medium clay, shale, and gravel; clay-cutter drag bits for cohesive soils; and spherical tungsten carbide (TC) button bits for hard, abrasive sandstone, quartz, and igneous granite formations. Custom diameters (from 42 mm up to 250+ mm) and customized flushing port configurations are tailored to your geotechnical borehole specifications.
Every export consignment is accompanied by comprehensive EN 10204 Type 3.1 Mill Test Certificates. Testing protocols cover heat chemical spectral analysis, continuous tensile yield and ultimate strength, percentage elongation, Charpy impact toughness at calibrated temperatures, thread dimensional gauge validation, and salt-spray corrosion chamber reports (ASTM B117) for galvanized and coated products.
Standard inventory sizes (such as R25, R32, R38, and R51 in 2 m, 3 m, or 4 m lengths) maintain rapid dispatch availability within 7 to 10 working days. Custom lengths, specialized metallurgy, or heavy micropile profiles (T76, T111) generally require 15 to 25 days production lead time. Typical MOQ starts at 5 to 10 tonnes for standardized products to optimize ocean container payload economics.
Specialized Heavy-Duty Bolts & Structural Components
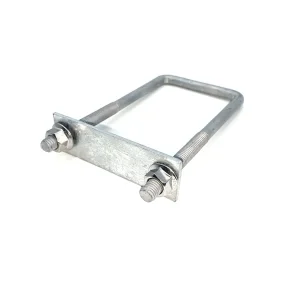
Explore additional factory-direct fastening systems engineered to complement anchor plates, purlin connections, and structural sub-assemblies.