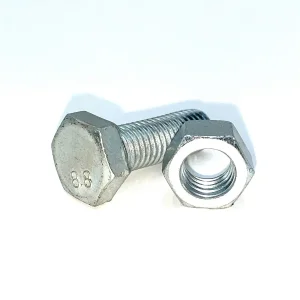
Factory-Engineered PV Mounting Hardware & Heavy Fastening
Explore our precision-manufactured structural hardware, hot-dip galvanized assemblies, and PV installation components engineered for rigorous industrial duty.



The Engineering Evolution of Long Galvanized Bolts
Examining the structural mechanics, corrosion dynamics, and metallurgy behind large-diameter, extended-length structural bolts across global civil and energy developments.
Extended Grip Length & Bending Fatigue
Modern mega-structures, utility-scale photovoltaic tracker arrays, and heavy timber-concrete composites mandate extended-length bolts (200mm to beyond 1,200mm). Unlike short fasteners, long galvanized bolts endure complex combined loading: continuous axial pre-tension coupled with severe lateral shear and cyclical dynamic bending moments caused by aeroturbulence and seismic frequencies.
Advanced Hot-Dip Galvanizing (HDG)
Standard electroplating (5-12µm) falls drastically short in open-air industrial settings. Advanced metallurgical Hot-Dip Galvanizing (per ASTM A153 Class C and ISO 10684) forms true metallurgical iron-zinc alloy layers (Gamma, Delta, and Zeta phases) capped by a pure Eta zinc outer barrier, providing 65µm to 100µm+ coating depth capable of resisting galvanic corrosion for over 30 to 50 years.
Tight Microstructure & Grain Alignment
Long structural bolts produced via continuous high-speed multi-station warm forming and CNC precision machining exhibit unbroken axial grain flow lines. This eliminates internal micro-voids, providing superior Charpy V-notch impact toughness (meeting ISO 898-1 standards even at sub-zero temperatures down to -40°C), making them impervious to sudden brittle fracture.
Global Enterprise Procurement Dynamics: TCO & Risk Mitigation
How Tier-1 engineering procurement contractors (EPCs) and industrial distributors de-risk long galvanized bolt procurement across worldwide supply chains.
Mitigating Hydrogen Embrittlement in High-Strength Fasteners
A primary risk factor in purchasing high-strength long bolts (Grade 8.8, 10.9, 12.9 or ASTM A490/A354 BD) is delayed failure from hydrogen embrittlement. Acid pickling during pre-galvanization baths releases atomic hydrogen, which migrates into intergranular boundaries under high mechanical tensile stress. Leading international manufacturing protocol mandates rigorous mechanical descaling (shot blasting) or, when chemical pickling is unavoidable, immediate de-hydrogenation baking at 190°C to 220°C for a minimum of 4 to 8 hours prior to hot-dip immersion.
Precision Thread Tolerancing and Overtapping Dynamics
Because hot-dip galvanizing deposits an irregular zinc coating measuring between 40µm and 90µm onto the bolt threads, standard ISO 6g/6h clearances cause binding and thread galling during automated high-speed nut installation on job sites. Factory manufacturers must engineer overtapped internal threads (e.g., 6AZ or 6AX class tolerances per ISO 965-5 or ASTM A563 over-tapping schedules) combined with automated centrifugal spinning of molten zinc from external bolt threads immediately after withdrawal from the kettle.
Total Cost of Ownership (TCO) Equation: Fasteners represent less than 2.5% of structural project CapEx, yet improper bolt choices cause over 65% of catastrophic joint structural failures. Sourcing factory-certified long galvanized bolts eliminates field rework, retorque delays, and catastrophic legal liabilities.
China Factory 4.0: Yongnian's Supply Chain Resilience
How the Yongnian Fastener Industrial Cluster in Handan delivers unrivaled production capacity, rapid lead times, and digital quality assurance to international projects.
The Fastener Capital Advantage
Situated in Yongnian District, Handan City, our manufacturing plant operates in the heart of the world’s most concentrated fastener supply cluster. Upstream raw materials (prime structural wire rod from regional steel powerhouses such as HBIS and Xingtai Steel) are secured with zero freight lag, reducing input cost variance and shielding buyers from global commodity volatility.
Automated Multi-Station Forging
Equipped with advanced 5-station and 6-station multi-stage cold heading and hot-forging machinery, our production facilities process long shank blanks with diameters from M12 up to M64 and lengths extending to 1,500mm. Integrated PLC robotics govern heat parameters throughout continuous mesh belt quenching and tempering furnaces.
Eco-Friendly Closed-Loop Galvanizing
Modern ecological stewardship meets heavy industry: our automated galvanizing workshops utilize zero-emission waste-acid recycling, automated filtration chambers, and intelligent robotic centrifuge baskets that guarantee razor-sharp thread crests and consistent protective coatings without hazardous environmental discharge.
International Structural Bolt Standards Comparison
Mechanical benchmarks, standard dimensional parameters, and hot-dip galvanizing specifications for technical procurement teams.
| Standard / Grade | Material & Alloy | Nominal Size (Dia × Len) | Tensile Strength (MPa) | Yield Strength (MPa) | Surface Treatment | Applicable Sectors |
|---|---|---|---|---|---|---|
| ISO 898-1 Gr 8.8 | Medium Carbon Steel / Boron Alloy | M12 × 100 to M48 × 1200mm | 800 – 830 MPa | 640 MPa | HDG ISO 10684 (≥55µm) | Solar PV Trackers, Pre-cast Concrete |
| ISO 898-1 Gr 10.9 | 40Cr / 42CrMo Alloy Steel | M16 × 120 to M56 × 1500mm | 1000 – 1040 MPa | 900 – 940 MPa | Centrifugal HDG / Dacromet | Wind Turbine Towers, Bridge Girders |
| ASTM F3125 A325 | Carbon / Alloy Structural Steel | 1/2" to 1-1/2" × Up to 36" | 120 ksi (825 MPa) | 92 ksi (635 MPa) | ASTM A153 Class C | Heavy Industrial PEB Warehouses |
| ASTM F3125 A490 | High-Strength Alloy (4140/4340) | 1/2" to 1-1/2" × Custom Lengths | 150 ksi (1035 MPa) | 130 ksi (895 MPa) | Zinc-Flake / Special Geomet | Seismic Steel Moment Connections |
| DIN 6914 / EN 14399 | High Strength Quenched Steel | M12 × 80 to M36 × 800mm | 800 – 1000 MPa | 640 – 900 MPa | K1/K2 Calibrated HDG | High-Speed Rail Bridges & Cranes |
Localized Engineering Use-Cases & Environmental Demands
From desert thermal expansion cycles to high-salinity offshore wind environments, long galvanized bolts serve as critical load-bearing anchors.
Utility-Scale Solar Racking & Trackers
Ground-mounted photovoltaic farms in arid regions experience extreme diurnal temperature differentials of 45°C. These thermal shifts induce significant expansion and contraction cycles across continuous steel purlins and ramming piles. Our hot-dip galvanized long hex bolts, paired with torque-tension calibrated prevailing torque locknuts, prevent vibrational loosening caused by aerodynamic vortex shedding across panel arrays.
Coastal Marine & Offshore Substructures
For installations in ISO 12944 C4, C5, and CX extreme marine atmospheric categories, hot-dip galvanized long anchor bolts with extra-heavy zinc coatings (minimum 85µm to 120µm) provide sacrificial cathodic protection. In the event of minor scratches or micro-impacts during installation, the sacrificial zinc anode oxidizes to shield the core steel, eliminating structural failure risks.
High-Voltage Transmission Towers
Lattice electricity transmission towers and monopoles demand high-strength long bolts (DIN 7990 / ISO 4014) to connect heavy steel angle sections. Subjected to dynamic aeolian vibration, ice load accumulation, and severe seasonal crosswinds, our hot-dip galvanized tower bolts ensure high fatigue resistance and fail-safe clamping forces throughout decades of service.
Engineering Questions & Procurement Insights
Comprehensive technical answers to address critical quality verification, plating tolerances, and material performance specifications.
Factory Direct Precision Fasteners & Infrastructure Hardware
Review our supplementary line of structural hex bolts, industrial purlin connectors, and aluminum mounting accessories engineered for heavy construction duty.