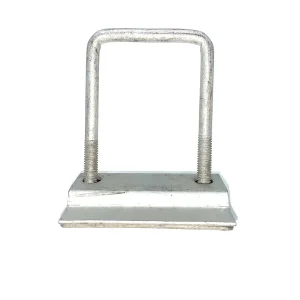
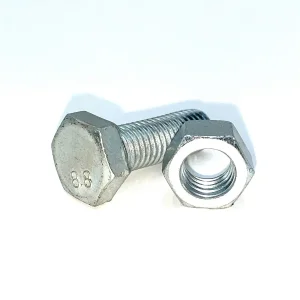
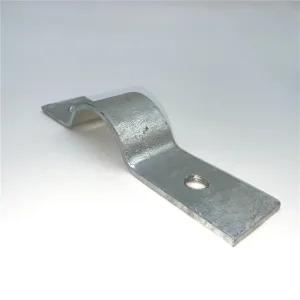
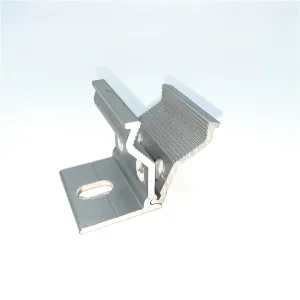
Featured Engineering Mounts & Industrial Anchors
Direct-from-factory structural hardware rigorously inspected for severe wind loading, high-vibration resilience, and verified anti-corrosive duty in international field conditions.





The Strategic Role of Anchor Bolts in Modern Macro-Infrastructure
Across global civil engineering, utility-scale photovoltaic arrays, and offshore wind development, structural fasteners serve as the definitive mechanical boundary between massive external kinetic stresses and the geotechnical foundation.
Severe Dynamic Loading Thresholds
Utility-scale solar structures encounter severe cyclic uplift dynamics and dynamic wind buffeting exceeding 160 km/h. Standard fastener anchor bolts must withstand multi-axis shear and tensile stresses without plastic deformation, requiring optimized metallurgical grain flow through precision hot-forging.
Atmospheric Environmental Degradation
Global renewable deployments are accelerating in hypersaline coastal regions, abrasive desert environments, and chemically aggressive industrial zones. Mechanical fasteners must eliminate galvanic electrolytic cells between aluminum superstructure rails and concrete base plates through advanced isolation and diffusion coatings.
Engineering Risk Amortization
Fastener hardware typically represents less than 3% of total project CAPEX, yet structural anchor failure accounts for over 45% of catastrophic civil and mechanical connection breakdowns during severe meteorological events. Tier-1 EPC contractors mandate fully traceable, batch-tested anchor bolts to protect multi-million dollar asset portfolios.
The Handan Industrial Cluster Advantage: High-Throughput Manufacturing & Scale
Located in the heart of Yongnian District, Handan, Hebei Province — universally recognized as the China Fastener Capital — our facilities leverage vertically integrated ecosystem synergies unmatched in the global fastener arena.
Immediate Raw Material Ingestion
Direct proximity to Hebei’s prime steel and metallurgical mills enables direct procurement of billet, cold-heading quality (CHQ) carbon steel, and certified austenitic stainless stock (AISI 304/316) without middle-tier transport markups or supply interruptions.
Automated Production Machinery
Continuous multi-station cold formers, automated high-tonnage stamping systems, CNC multi-axis machining cells, and robotic thread rolling ensure absolute thread dimensional tolerance compliance under ISO 965 and ASME B1.1 standards.
Integrated Surface Treatment Lines
Continuous hot-dip galvanizing baths (HDG), automated zinc-nickel plating lines, and fluoropolymer coating facilities operating under strict environmental and chemical management systems guarantee uniform coating thickness without thread clogging.
Comprehensive Fastener Selection Matrix by Structural Environment
Premature structural breakdown frequently stems from metallurgical miscalculations under specific environmental corrosive stress. Refer to our verified laboratory guidelines based on ISO 9223 classifications.
| Installation Environment | Corrosive Category | Recommended Bolt Grade | Surface Treatment / Finish | Tensile / Proof Strength Profile |
|---|---|---|---|---|
| Inland PV Ground Mounts & Dry Civil Pours | ISO C1 – C2 (Very Low to Low) | Carbon Steel Gr 4.8 / 8.8, Q235B | Electro-Galvanized (12–15 µm) or HDG | Tensile: 400–800 MPa | Shear: High Elastic Limit |
| Commercial & Industrial Rooftop Solar | ISO C3 (Medium Urban/Light Acid) | Austenitic Stainless Steel A2-70 (AISI 304) | Passivated Clean Finish / Wax Coated | Tensile: 700 MPa | Yield: 450 MPa Continuous |
| Chemical Plants & Heavy Agricultural Facilities | ISO C4 (High Industrial Sulfur/Ammonia) | High-Tensile Gr 10.9 Carbon / A4-70 | Hot-Dip Galvanized (>85 µm) or Zinc Flake | Tensile: 1040 MPa | Elongation: Min 9% |
| Coastal Arrays, Near-Shore & Marine Civil | ISO C5-M (Extreme Salt Spray / Marine) | Marine Grade A4-80 (AISI 316) / Duplex 2205 | Electro-Polished / Fluoropolymer Barrier | Tensile: 800 MPa | High Pitting Resistance (PREN >25) |
| Heavy Seismic Foundation Basements & Anchor Cages | Dynamic Soil Contact / Concrete Sub-grade | Gr 8.8 / ASTM A325 Heavy Hex / ASTM F1554 | Hot-Dip Galvanized to ASTM A153 | Impact Charpy V-Notch: 27J at -20°C |
Galvanic Electrolysis Mitigation
Direct contact between aluminum mounting rails and stainless or carbon steel hardware sparks rapid galvanic pitting in humid air. We engineer bespoke EPDM and high-density polymer isolation shims that permanently isolate differing electrical potentials.
Seismic Shear Anchorage Engineering
Cast-in-place J-bolts and heavy foundation anchor studs require deep ductile embedment with engineered hook radii to ensure plastic necking occurs well before concrete pull-out cone fracture under high Richter seismic accelerations.
Torque-Tension Preload Calibration
Under-torqued assemblies loosen under wind turbulence; over-torqued fasteners suffer stress-corrosion cracking (SCC). Our technical teams provide certified torque specifications and thread lubrication solutions for all diameters.
Technological Innovations Shaping the Structural Fastener Horizon
The industrial fastener sector is transitioning from standard commodity manufacturing toward smart, micro-alloyed, and sensor-monitored fastening ecosystems driven by gigawatt-scale project economics.
Micro-Alloyed Lightweight Carbon Steels
By integrating micro-additions of Boron, Vanadium, and Niobium, next-generation Grade 10.9 and 12.9 anchor fasteners achieve enhanced tensile performance while avoiding hydrogen embrittlement hazards common in heavy zinc plating processes.
Eco-Friendly Chromium-Free Geomet Coatings
Replacing older electroplating regimes, non-electrolytic zinc-flake coatings provide over 1,500 hours of ASTM B117 neutral salt spray protection with ultra-thin layer deposition (5–8 µm), preserving precise internal thread fits without chasing.
Smart IoT Preload Verification Anchors
Sensory-embedded structural bolts featuring internal ultrasonic transducers enable maintenance teams to conduct instant wireless preload diagnostics across expansive solar fields, transforming costly manual retightening schedules into predictive digital telemetry.
Global EPC Procurement Criteria: Navigating Factory Audits & QA Protocols
Acquiring industrial fasteners at bulk scale demands verification of rigorous documentation standards to safeguard structural warranties and civil sign-offs.
1. Traceable Mill Test Certification
Never accept generic commercial invoices. Mandate EN 10204 3.1 Mill Test Certificates (MTC) detailing original melt furnace ladle chemistry, verified tensile tests, yield strength parameters, elongation rates, and Brinell/Rockwell hardness mapping.
2. Empirical Salt Spray Verification
Ensure independent laboratory compliance reports under ASTM B117 or ISO 9227. Accelerated cyclical corrosion test chambers must validate zero red rust formation at agreed-upon project exposure thresholds (e.g., 720h, 1000h, or 1500h).
3. Batch Dimensional Tolerancing
Utilize optical laser-sorting and ring-gauge inspections for 100% thread profile accuracy (6g / 6H fit). Inconsistent pitch diameters produce severe galling on job sites, leading to equipment failure during high-speed impact-driver installation.
Industrial Fastener & Structural Anchor Clarifications
Clear answers to complex technical and logistical inquiries frequently posed by EPC structural leads, procurement teams, and plant managers.
What are the key technical differences between mechanical expansion anchor bolts and cast-in-place anchor studs?
How does Handan Youlong Fastener avoid galling (cold welding) in stainless steel PV bolt assemblies?
What quality standards govern the hot-dip galvanizing process for external anchor bolts?
Can Handan Youlong manufacture custom anchor bolts according to engineering CAD/BIM blueprints?
What documentation accompanies export shipments for customs clearance and engineering sign-off?
Specialized Photovoltaic Hardware & Heavy Fastening
Explore our complementary assembly components, mounting clamps, structural purlin connectors, and high-tensile hardware engineered for demanding industrial builds.