
Featured Industrial Mounting & Fastening Solutions
Engineered for extreme environmental exposure, solar utility structures, civil masonry, and heavy structural connections. Sourced directly from our advanced production facilities.

China High-Strength Aluminum Alloy Solar PV Mounting Base - Durable Support from China Suppliers
View Specifications →
China High-Strength Stainless Steel Hex Socket Cap Screw - China Suppliers Factory for Machinery
View Specifications →
Buy High-Quality Stainless Steel Carriage Bolt Suppliers in China - Durable Fasteners for Construction
View Specifications →
Buy High-Quality Aluminum Angle Bracket for Solar PV Mounting - Reliable China Suppliers & Factory
View Specifications →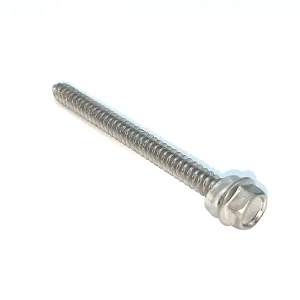
China High-Quality Stainless Steel Self-Drilling Screws from China Suppliers - Fast Installation
View Specifications →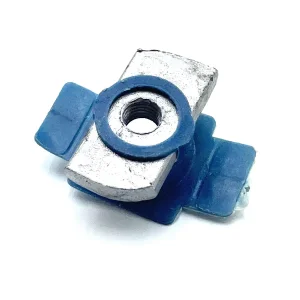
China Plastic Wing Nut Suppliers, Factories - Lightweight Non-Conductive Fastening Solutions
View Specifications →
Buy China Factory Suppliers Heavy-Duty Stainless Steel Expansion Bolt for Concrete & Brick Wall Fixing
View Specifications →
Best High-Strength Solar PV Mounting Aluminum Alloy Base - Reliable Support from China Suppliers
View Specifications →Engineering Integrity: The Metallurgy of Mechanical Galvanization
Evaluating why leading global engineering and procurement contractors (EPCs) mandate mechanically galvanized fasteners for critical high-tensile structural infrastructure.
Absolute Elimination of Hydrogen Embrittlement
High-strength bolts (Grade 8.8, 10.9, ASTM A325, A490) suffer catastrophic brittle fractures when exposed to acid pickling and cathodic electro-reactions. Mechanical galvanizing uses physical peening with specialized glass beads in a cold chemical bath, guaranteeing zero hydrogen absorption.
Micron-Level Uniformity Across Threads
Hot-dip galvanizing causes molten zinc pooling in the root of external threads and clogging in internal threads, requiring destructive re-tapping that strips corrosion protection. Mechanically applied zinc provides identical coating thickness from root to crest across intricate pitches.
Superior Torque-Tension Predictability
The mechanical consolidation of zinc, tin, and aluminum powders yields a controlled friction coefficient (k-factor). Structural bolting assemblies achieve stable tension targets without galling, thread galling, or unpredictable nut friction during high-speed pneumatic assembly.
Standards Compliance Matrix: Our mechanically galvanized structural fasteners are manufactured and tested in strict accordance with ASTM B695 (Standard Specification for Coatings of Zinc Mechanically Deposited on Iron and Steel), ASTM A153/A153M Class C equivalents, ISO 12683, and EN ISO 10684 compatibility criteria.
| Evaluation Parameter | Mechanical Galvanizing (Our Factory) | Hot-Dip Galvanizing (HDG) | Electro-Galvanizing (Zinc Plating) |
|---|---|---|---|
| Process Temperature | Ambient (Cold Peening, 20°C - 30°C) | Extreme Heat (450°C - 480°C) | Ambient (Chemical Electro-Bath) |
| Hydrogen Embrittlement Risk | Zero (Non-Acid Chemical Clean) | High on Class 10.9+ / Requires Post-Bake | Severe Risk on High-Tensile Steels |
| Coating Thickness Uniformity | Uniform across roots, crests & cavities | Irregular; meniscus pooling in thread roots | Thin on recesses, thick on edges |
| Need for Thread Chasing/Re-tapping | No Re-tapping Required | Mandatory over-tapping of nuts (loss of coat) | Not required due to thin layer |
| Typical Thickness Range | 8 µm up to 110 µm (ASTM Class 5 to 110) | 45 µm to 85 µm (Variable) | 3 µm to 12 µm (Low outdoor longevity) |
China Factory 4.0: Handan Fastener Capital Supply Architecture
Operating at the epicenter of global fastener manufacturing, our integrated production ecosystem in Yongnian, Handan, solves global procurement choke points through scale, agility, and end-to-end quality sovereignty.
Direct Mill Integration & Raw Material Sovereignty
Located within 50 km of China's premier specialized steel mills, our plants secure verified carbon steel coils (10B21, 35CrMo, 42CrMo, SCM435) with complete heat-number traceability. This eliminates raw material price volatility and provides raw steel batches with certified chemical compositions.
Automated Multi-Station Cold Heading Lines
Our manufacturing floor runs continuous 5-station and 6-station high-speed cold heading formers capable of producing standard hex flange, carriage, heavy hex, and customized socket fasteners up to M36 dimensions with dimensional tolerance windows restricted to ±0.02 mm.
Closed-Loop Environmental Mechanical Plating
Unlike heavy hot-dip galvanizing plants facing frequent carbon quota restrictions and shutdowns, our automated mechanical tumbling units run on clean electrical energy with 98% water reclamation and zero toxic metal fumes, guaranteeing uncompromised year-round delivery schedules.
Global Procurement Needs Across Solar, Wind & Heavy Civil Works
International EPC firms are transitioning their bill of materials (BOMs) from conventional zinc electroplating and hazardous hot-dip coatings to mechanical galvanization.
Utility-Scale Photovoltaic Ground Mounts & Trackers
Modern solar farms operate in harsh microclimates, from hyper-saline coastal shores to hot, corrosive desert dust bowls. Mechanically galvanized class 55 bolts withstand harsh C4/C5 atmospheric classifications. When torqued onto extruded aluminum rails, mechanical zinc mitigates galvanic couples far more effectively than bare stainless steel, eliminating accelerated bimetallic corrosion.
High-Vibration Wind Power Tower Assemblies
Wind turbine nacelles, platforms, and secondary structural brackets endure dynamic cyclical fatigue. Mechanically galvanized grade 10.9 structural bolts offer fatigue limits identical to uncoated substrate steel because the process avoids the thermal shock, temper softening, and micro-cracking induced by 460°C molten zinc immersion baths.
Civil Transport & Bridge Infrastructure
Highways, guard rails, noise barriers, and overpass seismic expansion joints require tension-critical fasteners that permit smooth robotic or pneumatic wrench installation. The precise thread tolerance of mechanically galvanized bolts prevents cross-threading, galling, and unexpected field torque rejection.
Seismic Heavy Expansion & Masonry Anchoring
When anchoring heavy equipment, structural columns, and base plates to cured concrete foundations, wedge anchors and fish-scale expansion bolts rely on calibrated sleeve expansion. Mechanically galvanized surfaces deliver uniform lubricity and thickness, ensuring verified pull-out strength without sleeve slippage.
Certified Testing, Metrology, and Verification Protocols
Under Google E-E-A-T and international ISO/IEC 17025 testing guidelines, every production heat run is subjected to rigorous destructive and non-destructive laboratory examination.
1. Magnetic & Eddy-Current Metrology
Non-destructive electromagnetic thickness gauges examine coating density across bolt shanks, hex corners, and internal thread flanks in compliance with ASTM B499, verifying that your specified thickness class (e.g., M55 = 55 microns) is fully achieved.
2. Continuous Neutral Salt Spray (NSS)
In accordance with ASTM B117 and ISO 9227, batch samples undergo continuous exposure inside cyclic corrosion chambers. Mechanically galvanized hardware regularly surpasses 1,000 to 1,500 hours without red rust (ferrous oxide) breakthrough.
3. Axial Tensile & Proof Load Rig
Computer-controlled 600kN and 1000kN servo-hydraulic universal tensile testers verify ultimate yield strength, elongation at fracture, and proof load capabilities, certifying structural compliance with ASTM A325, DIN 6914, and ISO 898-1.
Frequently Asked Questions: Mechanically Galvanized Bolts
Clear, authoritative technical answers addressing metallurgical considerations, international shipping logistics, and custom manufacturing specifications.
What is the key difference between mechanical galvanizing and hot-dip galvanizing?
Hot-dip galvanizing (HDG) immerses steel into molten zinc at roughly 450°C, producing intermetallic iron-zinc alloy layers. This extreme heat can cause temper softening in high-strength bolts (Grade 10.9/Grade 8) and creates risk of hydrogen embrittlement during pre-dip acid pickling. Mechanical galvanizing applies pure zinc powder cold in a tumbling drum via glass bead peening, completely eliminating heat distortion, thread bridging, and hydrogen entrapment.
Why do ASTM A490 and Class 10.9 fasteners prohibit hot-dip galvanizing?
Structural standards such as ASTM A490 explicitly forbid hot-dip galvanizing due to the dangerous probability of Hydrogen Embrittlement (HE) and Stress Corrosion Cracking (SCC). Under structural tension, trapped atomic hydrogen migrates to grain boundaries, leading to sudden, catastrophic bolt snapping without warning. Mechanical galvanizing (under ASTM B695) is the primary globally approved method to provide heavy protective zinc coatings on ultra-high-strength steel bolts without embrittlement risk.
Do mechanically galvanized nuts need to be tapped oversize?
Generally, no. Because mechanical deposition can be controlled precisely down to micrometer tolerances (such as Class 25 or Class 40), mating internal and external threads fit cleanly within standard 6g/6H or 2A/2B thread fit limits. For heavier deposits (Class 55 or Class 80), minimal overtapping or specialized thread gauging is utilized, preventing thread scraping or binding during on-site installation.
What is the typical lead time and minimum order quantity (MOQ) for custom bolts?
For standard sizes (M8 through M30; 5/16" through 1-1/4"), our automated lines support standard lead times of 15 to 25 days with an MOQ of 1 metric ton. For custom engineered OEM fasteners matching detailed 2D/3D customer blueprints, tooling and prototype samples are typically delivered within 7 to 10 days, followed by full container dispatch in under 30 days.
Industrial Brackets, Anchors & Solar Fastener Solutions
Explore our complementary range of high-durability expansion hardware, mounting connectors, and carriage bolts manufactured for industrial resilience.
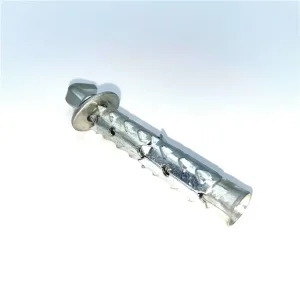
Best China Heavy-Duty Fish Scale Expansion Bolt - High-Stability Fasteners from Reliable Suppliers
View Specifications →
Buy China Suppliers High-Quality Solar PV Aluminum Alloy Angle Bracket - Durable and Lightweight
View Specifications →
China China Factory Premium Three-Hole Mounting Connector for Solar PV Systems – Top Suppliers
View Specifications →
China High-Strength Stainless Steel Hex Socket Cap Screw - Corrosion-Resistant Fastening Solutions
View Specifications →
China Heavy-Duty Hot-Dip Galvanized Carriage Bolt - China Suppliers & Factory for Robust Outdoor Solutions
View Specifications →
Buy China Solar PV Aluminum Alloy Angle Bracket | Durable Suppliers & Factory for PV Systems
View Specifications →
Best Premium Aluminum Side Clamp for Solar PV Panels - Top China Suppliers & Factory for Robust Solutions
View Specifications →
China Durable M-Type Aluminum Water Channel for PV Mounting Systems - Quality Factory Manufacturers
View Specifications →Partner Directly with China's Premier Mechanical Galvanizing Factory
Whether you require high-tensile structural bolting sets, OEM custom drawing fabrications, or certified corrosion-resistant mounting assemblies for utility infrastructure, our engineering desk is equipped to review your requirements with comprehensive mill test certificates (MTR) and salt spray reports.